Why Do Stamped Parts Develop Incomplete Edge Separation and Excessive Burrs?
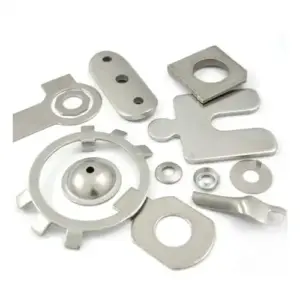
During metal stamping production, incomplete separation of the cut material and excessive burr formation are common issues that can affect part quality, assembly, and downstream processes.
When a customer recently asked why stamped components may not separate cleanly during production, our engineering team identified several potential causes related to die clearance, die shut height, and scrap-cutting geometry.
Understanding these factors is essential for maintaining stable production and consistent edge quality.
1. Incorrect Punch-to-Die Clearance
One of the most common causes of incomplete material separation and excessive burrs is incorrect punch-to-die clearance.
In blanking operations, the final part dimensions are primarily controlled by the die opening, while in punching operations, the hole dimensions are primarily controlled by the punch. The required clearance between the punch and die must be carefully selected according to the material type, thickness, hardness, and process requirements.
If the clearance is too large or too small, the material may not fracture properly along the intended shear zone. This can result in incomplete separation, excessive burrs, dimensional variation, or accelerated tool wear.
When a die component is damaged and requires repair, the repaired area must be accurately re-established. Depending on the tooling structure, repair may involve welding and subsequent CNC machining, followed by precision machining of the mating punch or die component using the repaired feature as a reference.
For high-precision stamping, maintaining accurate punch-to-die clearance throughout the tooling life is critical to consistent cutting quality.
2. Incorrect Die Shut Height or Press Setup
Die shut height is another important factor affecting stamping performance.
During die tryout and repair, engineers may need to make repeated adjustments to the die shut height or press setup parameters to eliminate product defects and achieve the required forming and cutting conditions.
If the shut height is not properly controlled, the upper and lower cutting components may not engage at the intended position. This can lead to incomplete cutting, excessive burrs, inconsistent part dimensions, or premature tool wear.
Once the required process parameters have been verified during tryout, the production settings should be standardized and documented for mass production. This helps ensure repeatability between production runs and minimizes unnecessary adjustments at the press.
3. Insufficient Scrap-Cutting Height or Poor Cutting Engagement
For precision stamping dies, the geometry and height of the scrap-cutting components also require careful control.
If the scrap-cutting section is too low or its height is insufficient, the upper and lower cutting edges may not achieve adequate engagement during the cutting operation. As a result, the scrap may not separate completely, leaving partially connected material or irregular edges.
Depending on the tooling design, corrective measures may include repairing or replacing the scrap-cutting component, adjusting its height, or modifying the mounting surface or support base to restore the required cutting engagement.
The exact corrective action should be determined based on the die structure, material thickness, and cutting conditions.
How to Prevent Incomplete Material Separation
To maintain stable cutting performance, stamping manufacturers should control several key parameters throughout the tooling and production process:
Proper punch-to-die clearance based on material type and thickness
Accurate die shut height and press setup
Correct alignment of upper and lower tooling components
Appropriate cutting-edge engagement
Regular inspection and maintenance of punches and dies
Controlled tooling repair and re-machining procedures
Standardized production parameters after die tryout
For precision metal stamping, these details can have a significant impact on edge quality, burr height, tool life, and overall production stability.
At Techsun, we focus on controlling tooling accuracy and process parameters throughout the stamping process to achieve consistent cutting performance and reliable part quality.