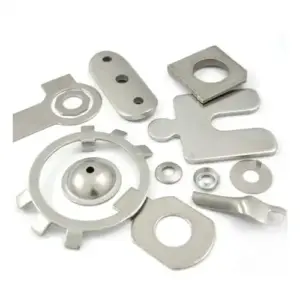
In custom aluminum stamping components, minimizing unplanned press downtime is essential for maintaining production efficiency, quality, and cost competitiveness. For high-volume manufacturing, even short interruptions can have a significant impact on overall productivity.
For this reason, effective stamping operations focus on three key objectives: reducing manufacturing costs, maintaining consistent quality, and improving production efficiency.
Many instances of press downtime can be traced to tooling issues, material feeding problems, setup errors, or quality abnormalities. By improving process control and paying close attention to these critical details, manufacturers can reduce unnecessary downtime and maintain more stable production.
1. Ensure Stable Material Feeding
Before starting the stamping process, the material feeding system should be properly set up and verified.
For coil-fed production, the strip must enter the die smoothly and consistently, with correct feed pitch, alignment, and tension. Material misalignment or unstable feeding can lead to dimensional variation, forming defects, die damage, and unplanned press stoppages.
For aluminum stamping, particular attention should also be given to material handling and surface protection, as aluminum is relatively soft and can be susceptible to scratching, deformation, and surface damage during feeding.
2. Maintain Effective Scrap Removal
Efficient scrap removal is essential for continuous stamping production.
Scrap generated during punching, blanking, trimming, or forming must be removed from the die area promptly and reliably. Accumulated scrap can interfere with the tooling, damage die components, obstruct material feeding, and create safety or quality risks.
The scrap discharge path should therefore be considered during die design and verified during production setup.
3. Prevent Material Misalignment
Material alignment is another critical factor in stable stamping production.
If the strip or blank shifts, tilts, or deviates from the intended position, the part may be formed or cut incorrectly. In severe cases, material misalignment can cause punch and die interference or even damage the tooling.
Proper guide systems, feed mechanisms, sensors, and process checks can help maintain accurate material positioning throughout the production cycle.
4. Monitor Feed Progression in Progressive Stamping
For progressive die stamping, accurate feed progression is critical because multiple operations are performed sequentially within the same die.
The strip must advance by the specified pitch at every cycle. If the material does not reach the correct position, the process should be stopped or corrected before further production continues.
Operators and engineers should monitor key parameters such as feed pitch, strip position, pilot engagement, and part transfer throughout the production process. Early detection of feed deviations can prevent larger quality problems and reduce the risk of tooling damage.
5. Establish Clear Scrap-Handling Procedures
Operators should clearly understand the intended direction and method of scrap discharge before production begins.
Scrap should be removed through the designated discharge system rather than manually interfering with the die during operation. Proper scrap-handling procedures help maintain production continuity, reduce the risk of tooling interference, and improve workplace safety.
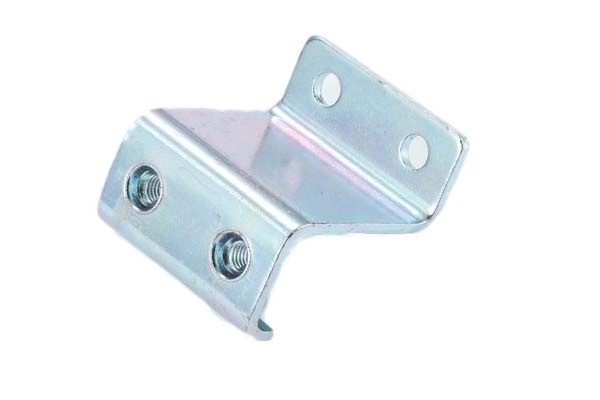
For aluminum stamping and deep drawing, where material behavior and surface quality can be particularly sensitive, preventive process control is essential to maintaining stable production.
By identifying potential sources of downtime before they become production problems, manufacturers can improve equipment utilization, reduce scrap and maintenance costs, and achieve more consistent production performance.
At Techsun, we focus on process stability and preventive control throughout stamping production to help customers achieve reliable quality, efficient manufacturing, and consistent delivery performance.