Explore Techsun’s metal manufacturing case studies, including precision metal stamping, progressive die stamping, deep drawing, sheet metal fabrication, and custom enclosure projects manufactured for OEM and industrial applications.
Metal Stamping Case Studies
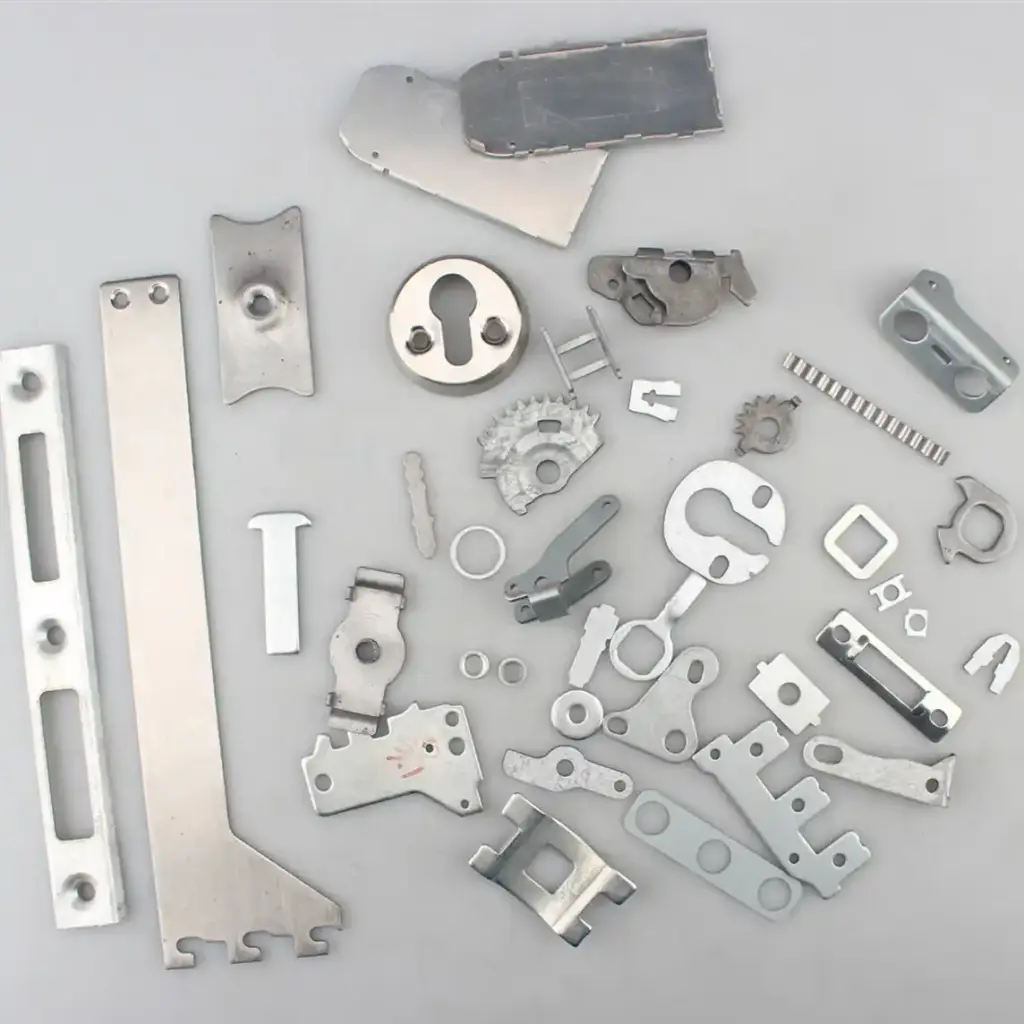
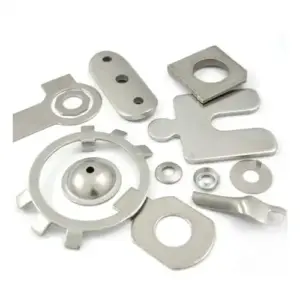
Precision Stamped Parts
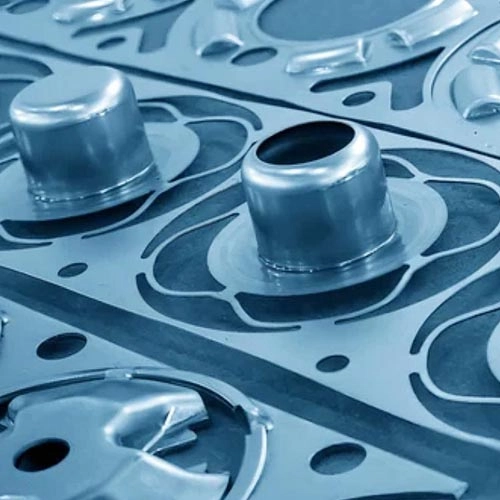
Progressive Die Stamping
Deep Drawn Metal Parts
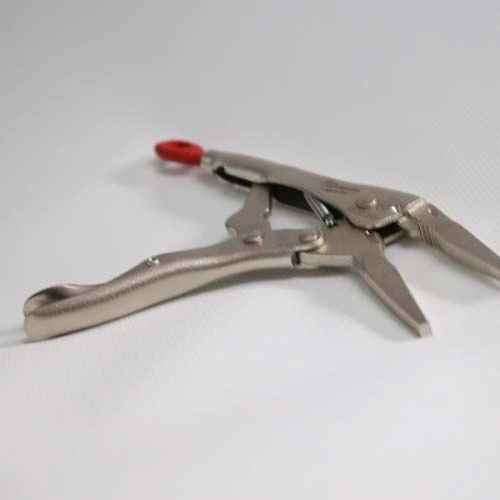
Hand Tool / Pliers Stamping
EV Copper Contact Stamping
Sheet Metal Fabrication Case Studies
Brand Client Case Studies: With over a decade of expertise in the sheet metal manufacturing industry, we have earned the trust of partners such as Ergsen, Hettich, and Spectrum Brands. We provide end-to-end, one-stop solutions encompassing Progressive Die Stamping Capabilities production design, customized Deep Drawn Stamping Services, and logistical support.
A kitchen and catering equipment customer required a deep-drawn circular housing. The main challenge was severe material thinning and surface cracking at the bottom corners during the multi-stage drawing process.
Solution: The Techsun engineering team redesigned the process into a four-stage continuous deep-drawing procedure. By strictly controlling the blank holder force and using specialized deep-drawn grade (DDQ) stainless steel, we achieved uniform wall thickness. Result: A seamless, crack-free housing with excellent sealing performance was successfully delivered.
Aluminum Stamping
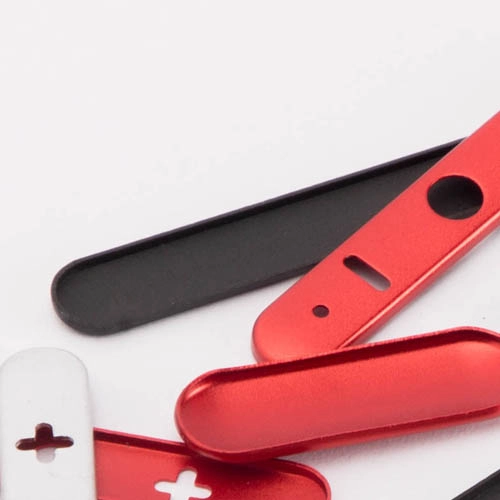
An electrical appliance customer required aluminum stamped parts. The main challenge was that the aluminum in the drawings was 1050, which is too soft and unsuitable for load-bearing or structural components in electrical appliances. Furthermore, soft materials are generally suitable for electrical and thermal conductivity in circuit boards.
Solution: Techsun’s engineering team proposed a new process and suggested that the partner adopt 5052 series aluminum, which is highly corrosion-resistant and of medium strength, using a 14-step continuous progressive stamping process. By strictly controlling the blank holder force and continuous stamping, we achieved mass production of aluminum products. Result: Successful delivery of product prototypes, small batches, and finally, large-scale production.
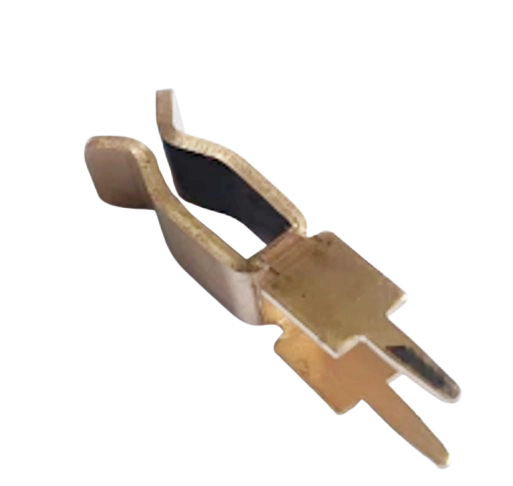
Copper Stamping
The customer faced challenges due to inconsistent contact pressure and non-compliance with tolerances caused by deformation and uncontrollable springback of standard materials.
Solution: Techsun optimized the mold process by modifying the die, using optimal machining, and employing heat-treated beryllium copper. We designed a custom progressive die with automatic over-bending compensation, ensuring extremely high tolerance control within ±0.02mm in batch production of over 1 million pieces. Result: Achieved 100% stable conductivity and completely eliminated defects on the customer’s assembly line.
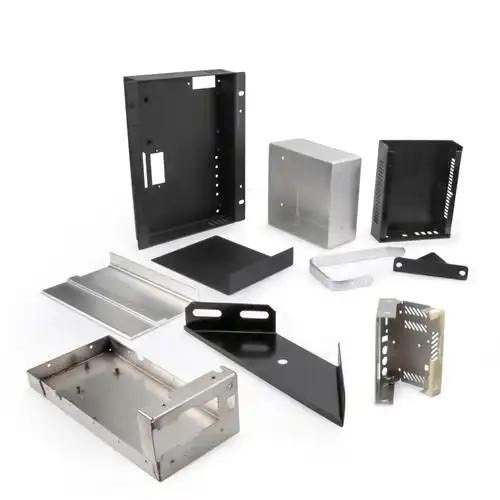
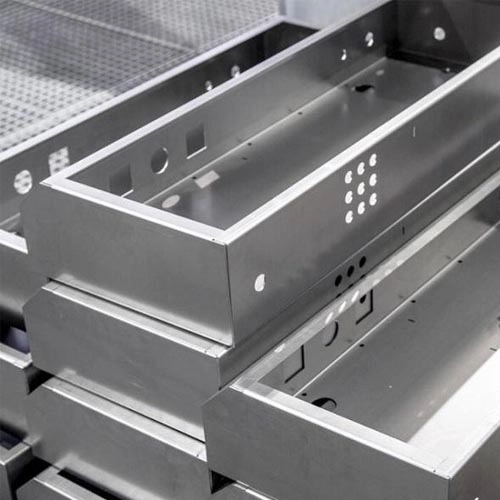
Sheet Metal Fabrication
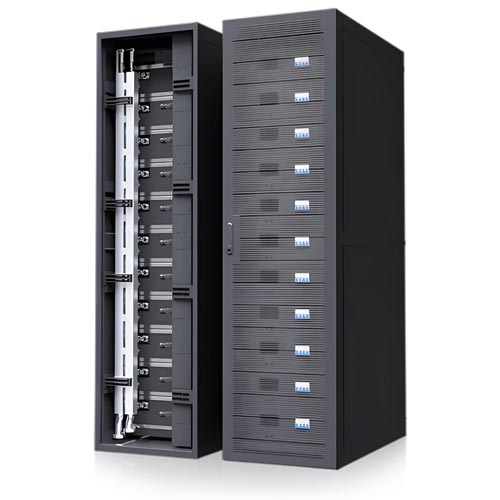
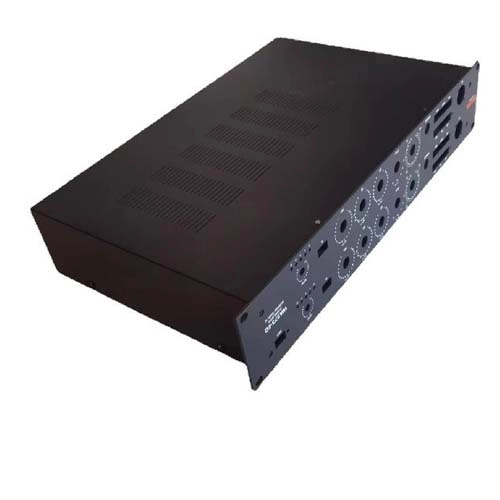
A partner hardware supplier required a custom chassis with a 75% ventilation rate while maintaining extremely high structural rigidity to withstand heavy server loads.
Solution: Techsun selected 5052 aluminum alloy to reduce weight, combining turret punching (for perfectly machined hexagonal ventilation mesh) with precision fiber laser cutting. Heavy-duty TIG/MIG welding was used to reinforce the structural corners, and finally, an anti-static powder coating was applied. Result: The overall shipping weight was successfully reduced by 20%, while fully meeting server heat dissipation and IP20 protection standards.
Contact us to explore more possibilities
You can contact our team and send us detailed information to receive a free quote. Our goal is to become your trusted partner and create endless possibilities.
One of the most troublesome issues we frequently discuss with structural engineers is the springback problem of steel in progressive dies, especially for materials like SUS304 or manganese steel. Over-bending or using special die geometries is key, but each geometry behaves differently.
To the engineers in my circle: In the DFM stage, before die opening, what are your preferred strategies for predicting and reducing steel springback? Do you rely heavily on simulation software, or do you still trust shop floor experience data more? Let’s discuss!
Trusted by OEM Customers
With more than a decade of experience in metal manufacturing, Techsun has supported customers across industrial equipment, hardware, electronics, and other OEM applications.
Have a Similar Project?
Send us your drawings, 3D files, specifications, or sample. Our engineering team can review your requirements and recommend the appropriate manufacturing process.